Key Takeaways
- Audit by route, not by checklist: walk production in order, and every station shows you the risk the next station inherits.
- The plush fault lines: shade matching at cutting, seam discipline at sewing, filling weight at stuffing, metal control at needle detection.
- Trust records over slogans — broken-needle logs, detector calibration cards, weighed filling shots.
- Needle detection is the station that cannot be faked while you watch; make the operator run a live test piece.
- Write every finding as photo, station, severity and deadline — findings without locations do not get fixed.
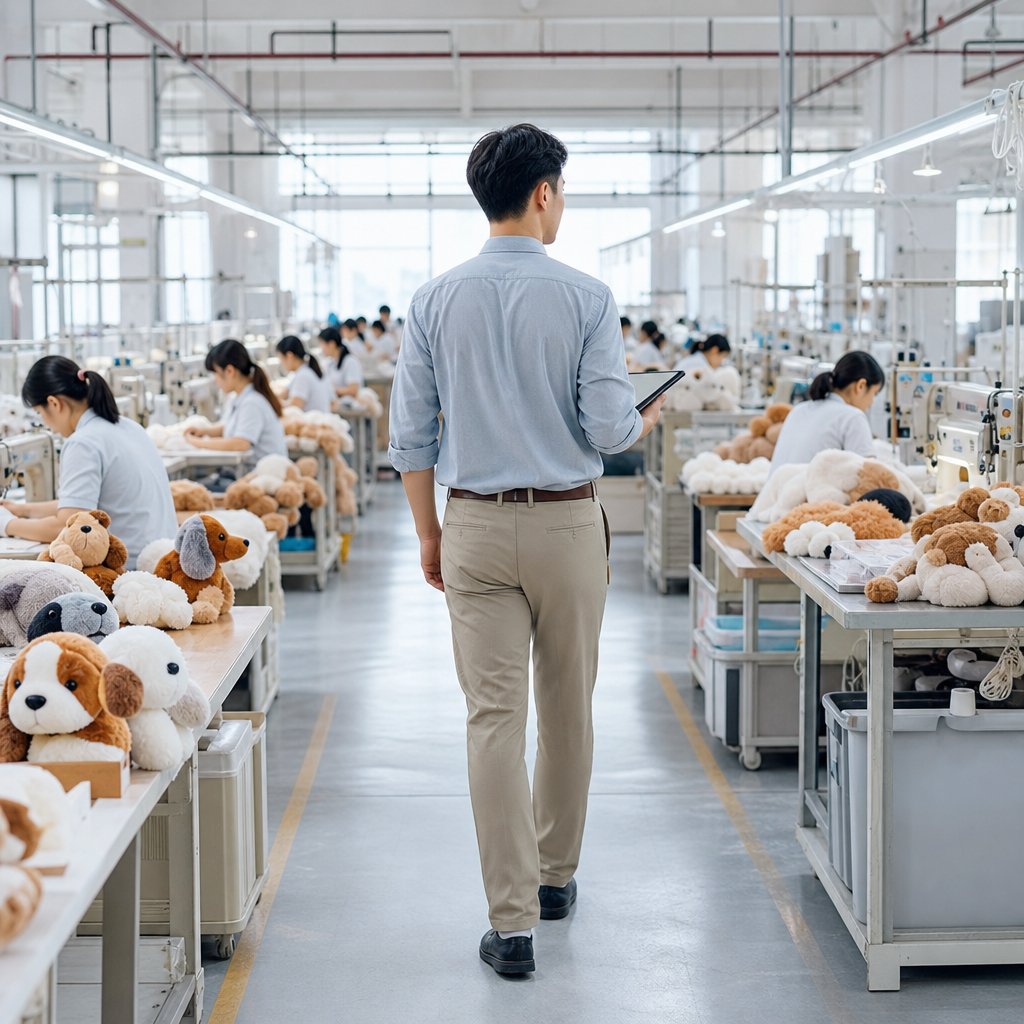
Most factory checklists fail the same way: they say what to look for, not where to stand. A factory expecting an audit can decorate a conference room with certificates in an afternoon. What it cannot stage in an afternoon is the sequence of its production flow — which is why the most informative audit is a walk, taken in the order the toy itself is made.
This article follows a plush pet toy through six stations, from the cutting table to the packed carton. At each stop: what to look at, what a red flag looks like, and the one question that moves the conversation.
Why the Route Beats the Checklist
A checklist is a list of objects; a route is a chain of causes. Audit in production order and each station explains the defects you will find at the next: fabric laid carelessly becomes shade mismatch in the finished toy; seam discipline lost at sewing becomes the open seam in a return photo; a skipped needle-detection pass becomes the metal fragment in a customer's complaint letter. Walking the route also exposes what no document shows — whether material flows forward only, or whether rework drifts back into the line without records. And it puts you in rooms where the manager's version of the factory has no influence over what is actually on the floor.
The Route at a Glance
Six stations, six defining risks:
| Station | What you look at | Red flag | Question that moves it |
|---|---|---|---|
| Cutting table | Lay height, shade bands, fur direction | Mixed lays from different dye lots | How are dye lots marked and segregated? |
| Sewing floor | Seam allowance, stitch density, rework flow | Unlabeled rework piles | Where does a failed seam go, physically? |
| Stuffing bay | Weighed filling shots, bay hygiene | Filling dosed by feel | Show me a worker weighing one shot. |
| Shaping and finishing | Trimming, brushing, eye and nose alignment | Loose plastic parts on worktables | How is attachment force checked? |
| Needle detection | Calibration, daily test pieces, broken-needle log | Log with gaps, no calibration record | Run a test piece for me now. |
| Packing line | Polybag warnings, carton specs, label match | Bags without warning print | Do packed counts reconcile to detection? |
The table is the skeleton. The sections below put muscle on the stations that decide most plush outcomes.
Cutting, Sewing and Stuffing: The Making Stations
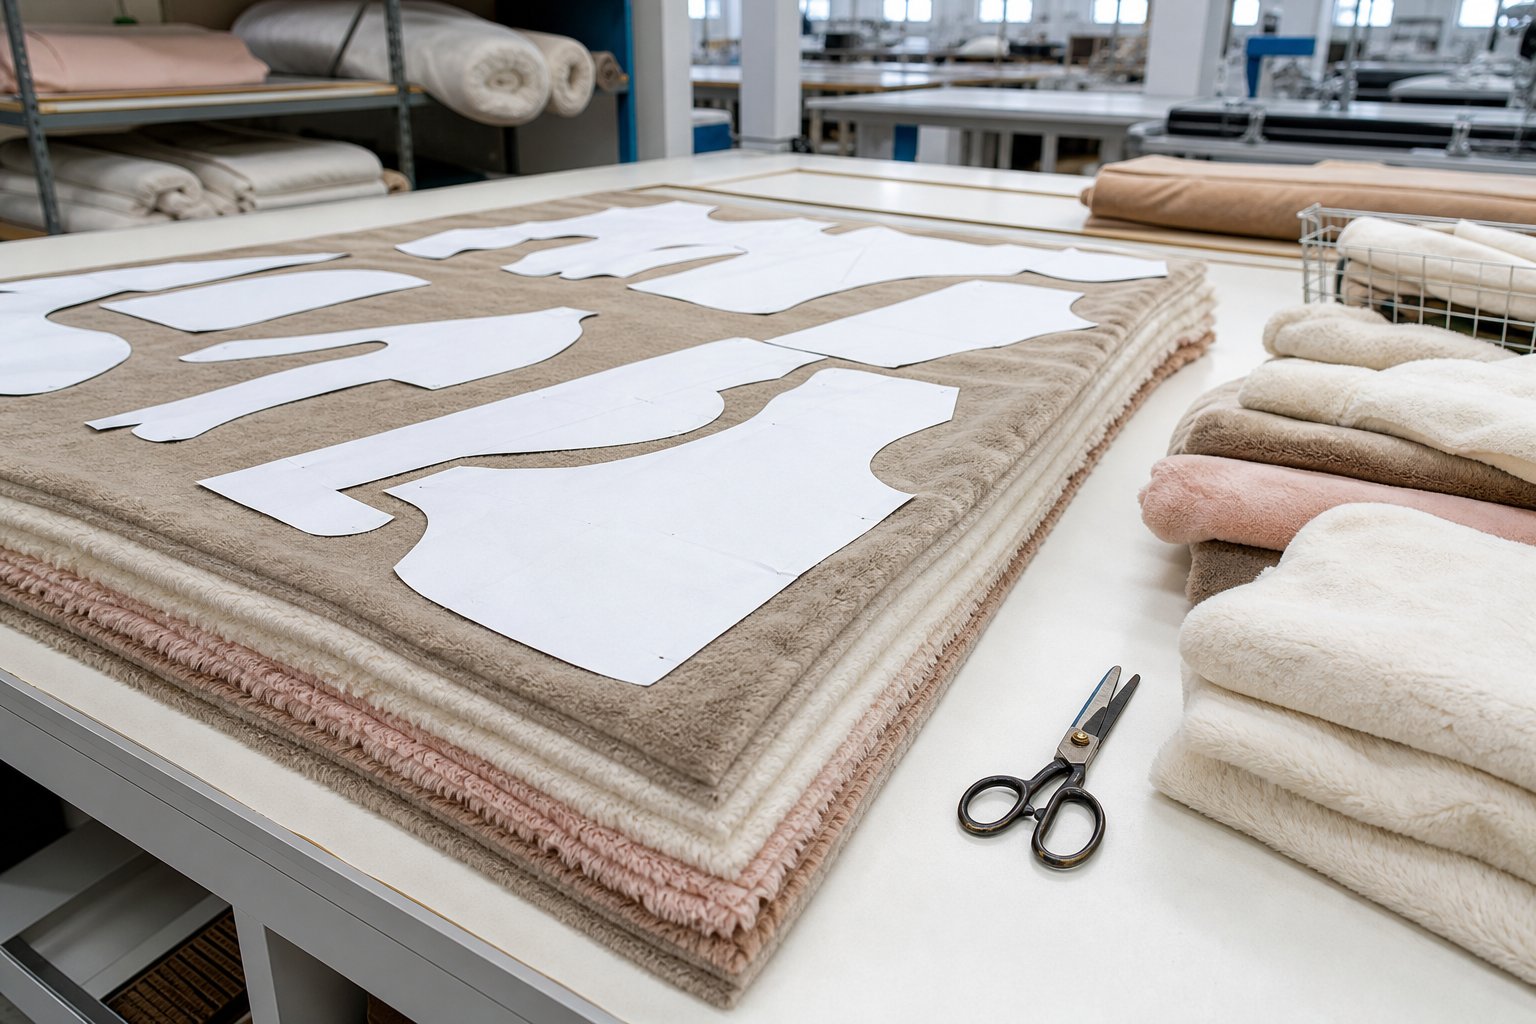
Cutting sets the ceiling on everything downstream. Look at how fabric is laid: the height of the lay, whether shade bands are kept separate, whether fur direction stays consistent within one pattern run. Shade banding — slight color drift between dye lots — is invisible in the lay and obvious in the finished toy, so the question is procedural: how are dye lots marked, and can the cutter hold a run inside one band?
At sewing, the discriminator is discipline, not skill alone. Check seam allowance consistency across operators, stitch density on the machines, and what happens to a failed seam — is there a labeled rework flow, or does a repaired toy slide silently back into the pile? Watch the in-line inspection point if one exists; a sewing floor without any intermediate check finds its defects at final inspection, where repair is costliest.
Stuffing is where weight and hygiene meet. Filling should be dosed by weight, not by feel — ask to see a worker weigh one shot. Under- and over-filled toys create the squashy inconsistency behind many returns, and an open filling bay invites the contamination that later shows up as stains and odor complaints.
Needle Detection: The Station That Cannot Be Faked
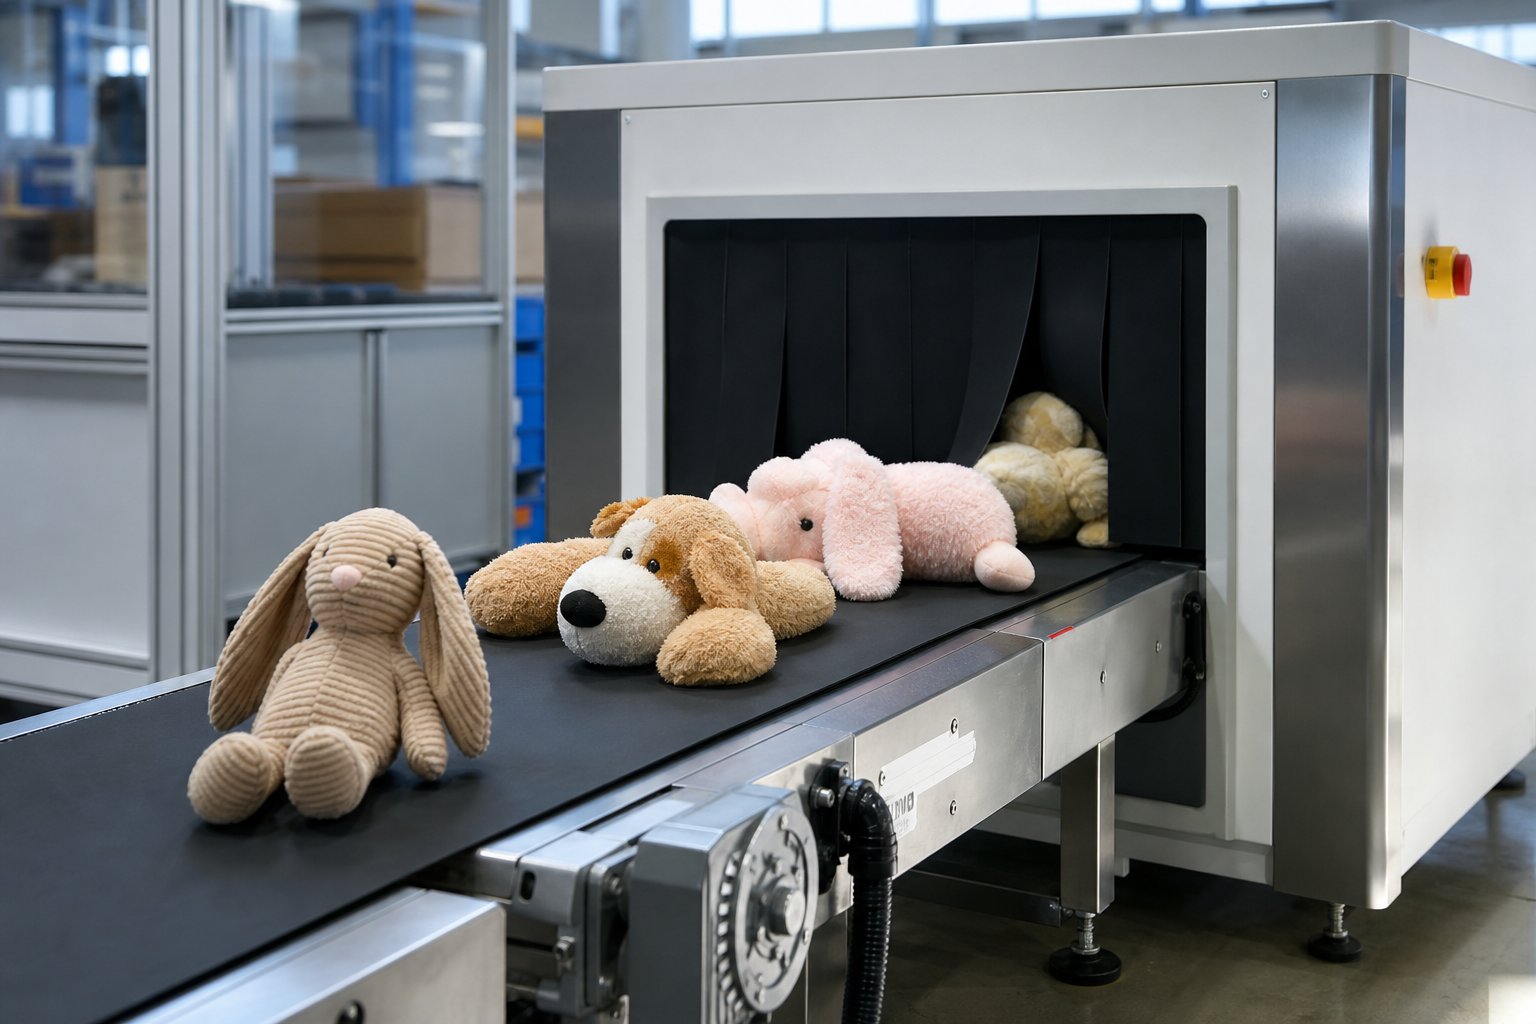
Broken needles are the plush industry's classic critical defect, and the control is procedural: every product passes a metal detector, every broken needle is logged, and the log reconciles against detection records. The audit move is to witness a live run — hand the operator a test card carrying a known ferrous fragment, watch the machine reject it, then ask for the week's log. Gaps in the log, test pieces that show no sign of daily use, or a detector without calibration records are not small findings; they mean the station is ceremonial. Also ask what happens to a rejected toy: it should be isolated and traced, not re-fed through the machine until it passes.
This is also where big-factory and small-workshop risk differ most. A small workshop may genuinely run without a detector — in which case the honest answer is outsourced detection or recorded hand-held scanning, not a shrug.
Packing Line and the Paper Trail
Packing is where compliance and logistics overlap. Polybags need warning print and the correct gauge; cartons need a drop-test history; labels need to match the order's language and destination. Then pull the thread backwards: does the packed quantity reconcile with the day's production and detection records? A packing line that reconciles belongs to a factory that knows what it made; one that estimates belongs to a factory you will be arguing with at claim time.
Records tie the route together. The strongest factories keep fabric intake logs, broken-needle logs at detection, and retained batch samples after packing — a chain you can follow with one finger during the audit. Where the chain breaks, write it down with the exact location.
Writing the Report So It Gets Fixed
An audit report fails when its findings are opinions. Give every finding four fields: photo, station, severity, agreed deadline. "Sewing quality needs improvement" changes nothing; "open seam, station 4, major defect, corrective sample by date" closes itself. Classify severity exactly the way you will classify it at shipment inspection, so audit language and inspection language stay identical — one defect catalog governing both, which is how golden samples and AQL defect classes keep their meaning between visits. Small factories deserve one adjustment: fewer stations does not mean less rigor — it means each finding carries more weight, so prioritize the two or three that matter and leave with committed dates.
Our factory page describes the production bases and lines behind our plush program; the route above is the same one our QC teams walk before any new program enters mass production.
Frequently Asked Questions
FAQ
How long should a first audit of a plush pet toy factory take?
Can an audit be done remotely over a video call?
What is the single most telling station on the route?
Should I audit before or after approving the sample?
Want suppliers who survive the walk before you take it?
Send your plush program — we will arrange a factory walk-through, live or on site, and share the station records before you commit to a deposit.