Key Takeaways
- Rubber chew toys are made in batches, not flows — what enters the mixer decides everything that leaves the press.
- Three parameters rule the press: temperature, pressure and time. Undercure and overcure fail in opposite ways.
- Odor and impurity problems are decided at the weighing scale, not at the packing table.
- Recycled content is the quiet variable: it moves cost, smell and PAH risk at once.
- Follow one lot number from scale to carton — traceability shown live beats any presentation.
The first decision about your chew toy is made before most of the factory has clocked in — at the weighing scale, in the compound room, where a recipe becomes a batch. Everything that follows, from the mill to the press to the trimming bench, is execution. That is why rubber factories reward a different kind of visit than sewing plants: the day has a rhythm, and the rhythm tells you whether quality is a system or a slogan.
Follow a working day in order — weighing, mixing, milling, molding, trimming, inspection — and note where buyers should look, what goes wrong at each beat, and which questions separate real control from theater.
A Batch Process, Not a Flow
Injection plants flow: resin in, parts out, one continuous ribbon. Vulcanized rubber plants pulse. A batch is weighed, mixed, milled into sheet, rested, then fed to presses that cure it under heat and pressure. Between batches the line changes personality — compound, color, hardness — which is precisely why batch discipline is the audit target. If a factory cannot show you where one lot ends and the next begins, it cannot tell you what went into the toys you already bought. The saving grace for visitors is that batch systems leave paper: weighing records, cure cards, retention samples. Your job is to ask for the paper while standing where it was written.
Weighing and Mixing: The Recipe Is the Product
The compound room decides most of what consumers will later describe as quality. A typical chew-toy recipe balances natural rubber, fillers, process oils, activators, curing agents and color masterbatch. Each line item moves something a buyer cares about: filler loading moves cost and rebound; the process oil moves odor and — if it is the wrong oil — PAH compliance; the curing package moves the press cycle; masterbatch moves color and, when cheap, heavy-metal risk. The quiet variable is recycled content. Legitimate regrind from controlled sources can be entirely reasonable; uncontrolled regrind is where smell and restricted substances concentrate.
On the floor, look for weighing discipline: recipes posted, scales calibrated, minor ingredients pre-weighed in labeled cups, batch tickets initiated at the scale. A compound room that eyeballs its minor ingredients will ship inconsistency, because nothing downstream can undo a mis-weighed cure package.
Mills and Sheets: Reading the Compound
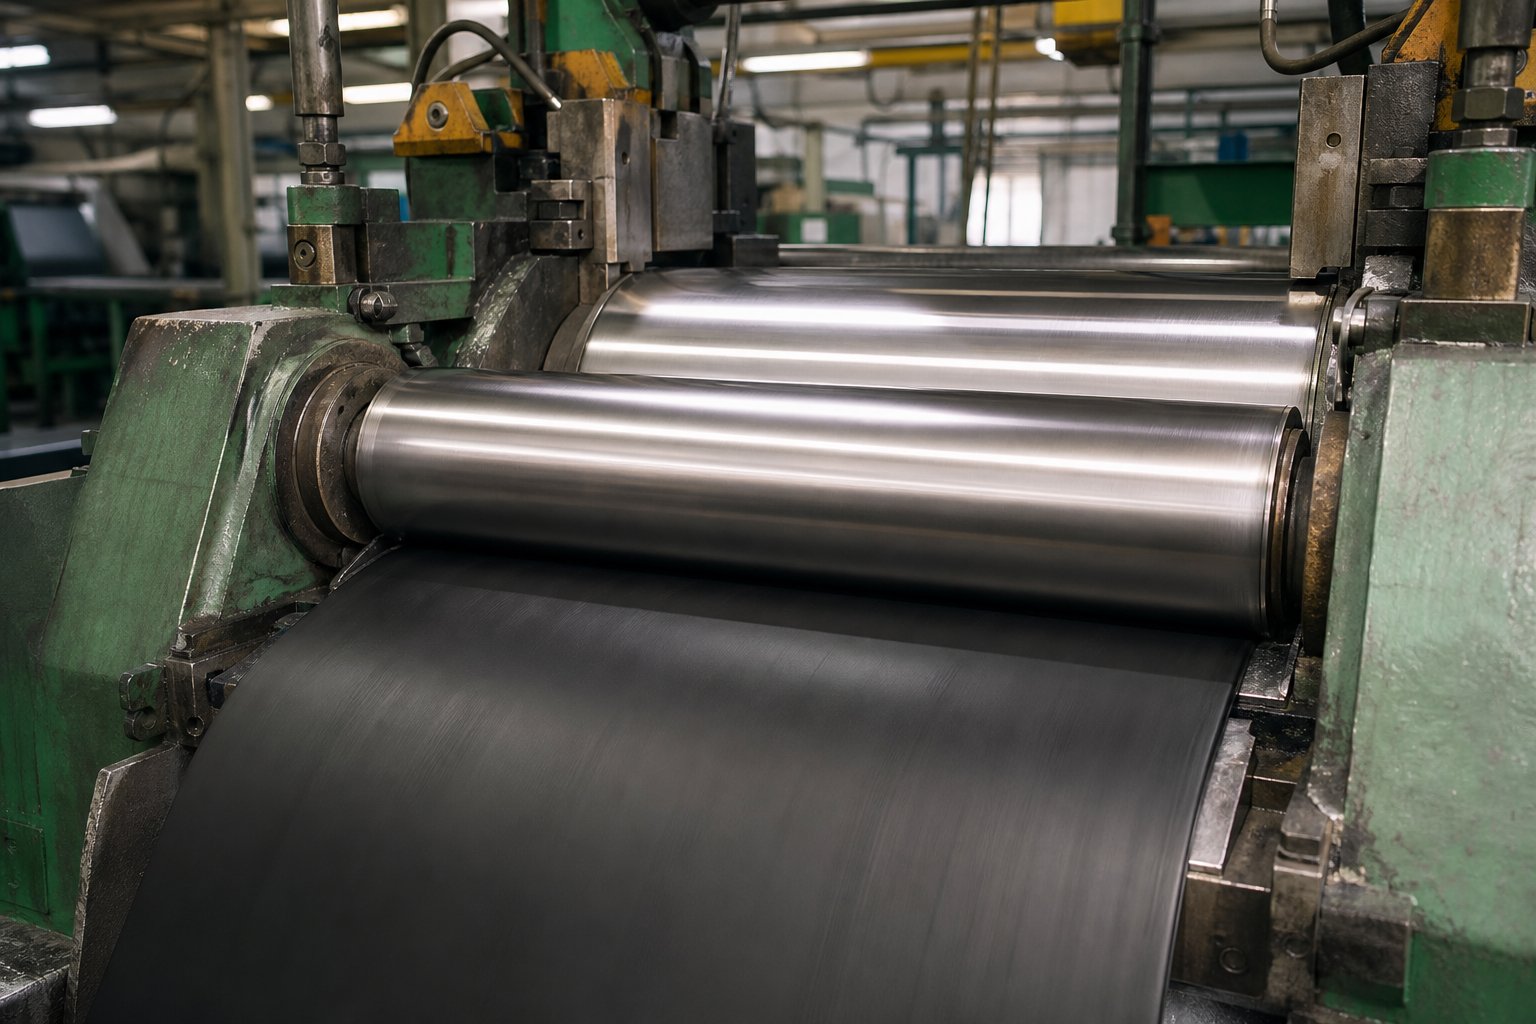
Mixed stock is worked on a two-roll mill into sheets, then rested before molding. This is the most tactile checkpoint of the day. A well-milled sheet looks uniform, matte and streak-free, wraps the roll smoothly, and smells faintly of rubber — not of solvents or scorched material. Streaks mean poor dispersion: color and additives unevenly spread, marbling its way into the finished toy. Sheets that feel tacky are starting to scorch, the compound's version of half-cooked dough, and scorched batches cure short and brittle at the press. Ask what happens to a streaked or scorched batch. Honest factories downgrade it to non-critical parts or scrap; the rest rework it quietly.
Molding and Vulcanizing: Temperature, Pressure, Time
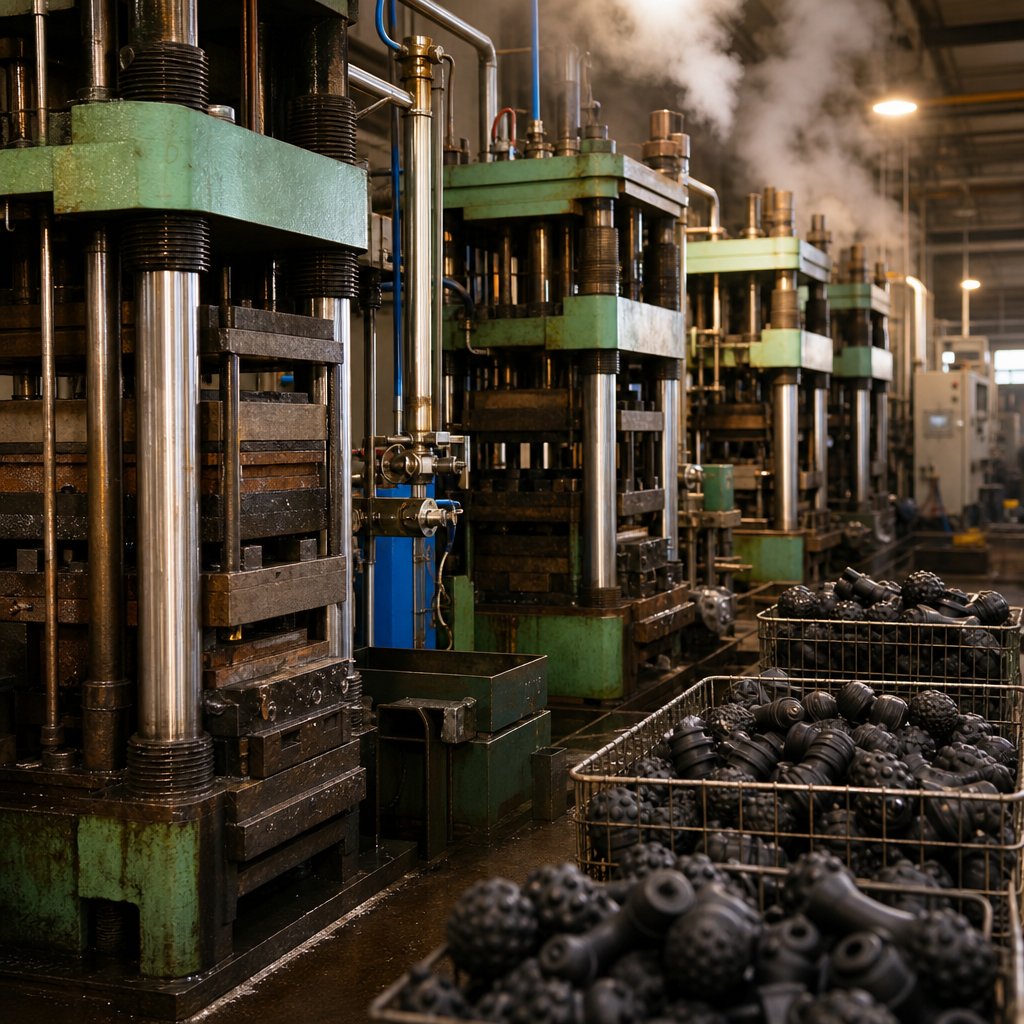
At the press, three numbers make the part: mold temperature, clamping pressure and cure time. Undercure leaves a toy that is tacky, slow to rebound, higher in residual odor and weaker in tear. Overcure buys dimensional stability at the price of rebound and brittleness — the toy that rings instead of squeezes. The craft is holding the window between them. Look for parameter cards at each press stating the cure window for the current recipe, first-article checks at shift start and after every batch change, and a written rule for what an operator does when scrap appears: adjust, flag, or stop.
Flash — the thin rubber escaping the mold seam — is normal; its fate is informative. Flash trimmed and sorted immediately suggests controlled flow. Bins of unmarked, mixed-color flash suggest regrind of unknown lineage heading back into future batches.
Trimming, Washing and the Afternoon Checkpoints
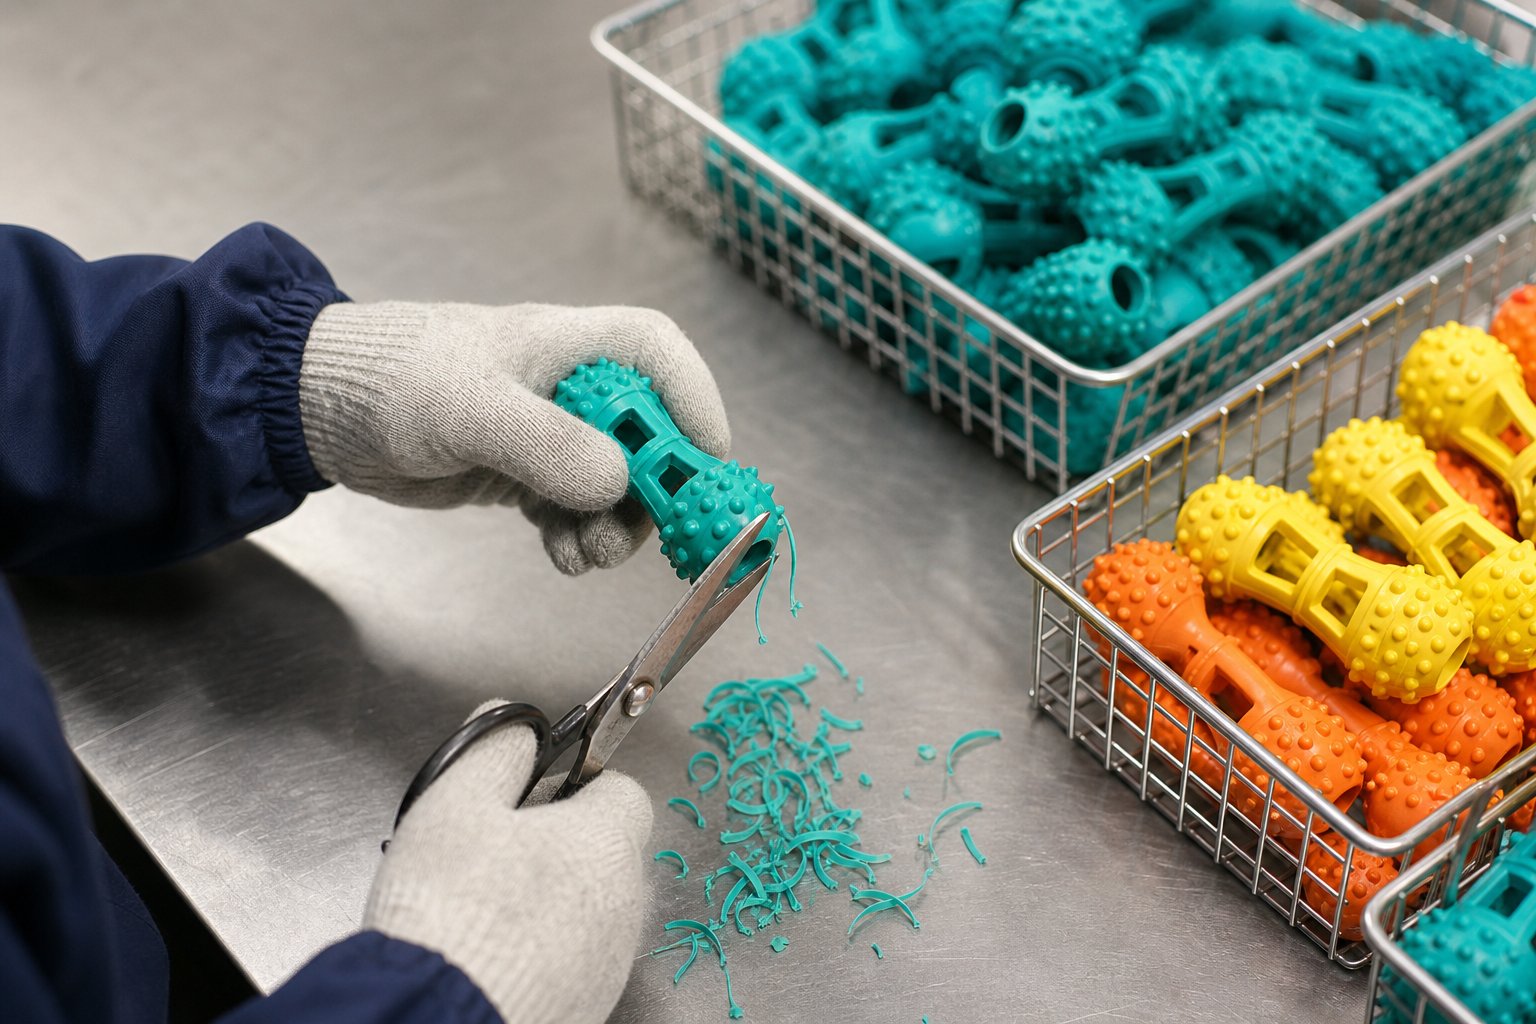
After cure, parts are deflashed, washed, aired and inspected. Trimming quality is the touch-point consumers judge first — a knife slip leaves a cut that reads in reviews as broke in a week. Washing removes mold release and dust; airing on open racks lets residual volatiles leave before polybags seal them in. Inspection then works under good light for impurities — embedded debris, porosity, foreign matter — and runs the batch sensory check: readings on the open toy, the rubbed surface and the sealed bag, compared against the approved reference. The afternoon's other quiet star is the retention shelf — kept samples per batch, dated, tied to the lot number that started at the scale.
The Visitor's Field Guide
Whether the visit is on site or through a camera, compress it into five beats:
| Step | What is controlled | What goes wrong | Buyer question |
|---|---|---|---|
| Weighing | Recipe accuracy, recycled ratio | Undocumented regrind | May I see one batch record? |
| Mixing and milling | Dispersion, uniformity, rest time | Streaks, scorch | Where does a scorched batch go? |
| Molding and vulcanizing | Temperature, pressure, time | Undercure, overcure | Who signs the first article? |
| Trimming and washing | Flash removal, residue | Cut marks, lingering odor | Where does the flash go? |
| Inspection and airing | Sensory grade, impurities | Rushed packing | Show me the retention shelf. |
Then follow one lot end to end. If the factory can walk you from a weighing record to a retention sample in ten minutes, traceability is a daily habit; if it needs a week to assemble the story, traceability runs for audits only. The factory page describes how our rubber and TPR lines are organized, and the same lot-level logic sits behind the odor control program and the batch sensory protocol we apply before shipment.
Frequently Asked Questions
FAQ
Why do identical-looking rubber toys differ so much in smell and strength?
Is natural rubber always better than TPR for power chewers?
How is odor controlled in rubber toy production?
What should I ask to see on a rubber factory visit?
Want to see the batch before it becomes your order?
Send your chew-toy program — we will walk you through the compound room and the presses, live or on video, lot by lot.